
SHEET METAL · PRODUCTION PLANNING
Sheet Metal Enclosure Production Case
How a formed sheet metal enclosure can move from validation to repeat production with fit-critical datums, finish protection and a practical inspection plan.
Representative manufacturing application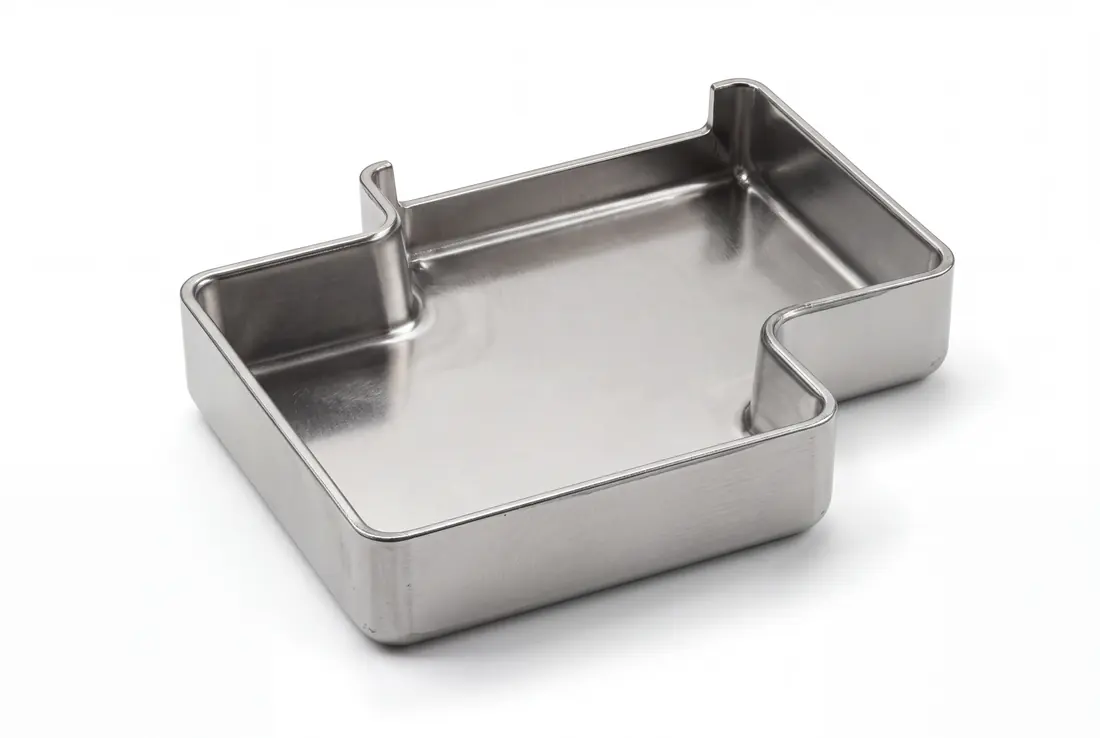
The manufacturing challenge
The brief starts with the finished part and its assembly requirements. Process and inspection choices follow those requirements rather than a generic tolerance claim.
The proposed production route
- 01
Resolve the formed geometry
Mark the assembly-facing tabs, corner form, and visible outside face. Review the blank and forming sequence before locking the drawing, with relief and edge treatment specified where needed.
- 02
Validate before dedicated tooling
Use trial blanks and formed samples to check access, fit, and surface appearance. If the volume forecast supports a dedicated tool, retain the validated datums and update the control plan for repeat output.
- 03
Release a complete part
Plan deburring, finish protection, hardware or joining if required, and packaging for the visible face. First-article and lot checks use the same drawing revision.
What the inspection plan needs to protect
- Tab position and formed height relative to assembly datums
- Corner form and flatness where the enclosure mates
- Burr direction, edge condition, and visible-face appearance
- Material and drawing revision identification for each lot
Outcome and engineering takeaway
Treat the enclosure as a finished assembly interface, not only as a flat blank. The important control points are identified before the process moves from flexible trials to repeat tooling.